Sourcing precision cnc machining parts can look straightforward until the first inspection report reveals a problem. A bearing bore measures 0.02 mm oversize, or a threaded hole fails its specified gauge check. Suddenly, a low unit price means little. Details matter. Manufacturing quality expert Joseph M. Juran defined quality as “fitness for use.” That principle applies directly to CNC sourcing: a component must satisfy its functional requirements, not merely resemble the drawing.
A supplier’s machine list offers useful clues, but it cannot establish process capability by itself. Ask how the shop controls critical dimensions, verifies material grades, and manages drawing revisions. For an aluminum housing, that might mean checking flatness after anodizing and confirming the inspection method before production. For a stainless steel shaft, surface finish and concentricity may determine whether the assembly runs smoothly. Request evidence. A sample inspection report, material certificate, and clearly documented acceptance criteria reveal more than broad promises about precision.
Even careful buyers make imperfect decisions. A flawless prototype does not guarantee consistent production, and an attractive quotation may omit finishing or inspection costs. Tight tolerances also deserve scrutiny; specifying them everywhere can increase cost without improving performance. The seven tips ahead cover drawing clarity, supplier capability, material traceability, inspection planning, sample approval, delivery reliability, and total cost. Together, they provide a practical basis for comparing suppliers and identifying questions worth resolving before issuing a purchase order. The goal is a sourcing decision supported by measurable requirements, credible records, and realistic expectations.
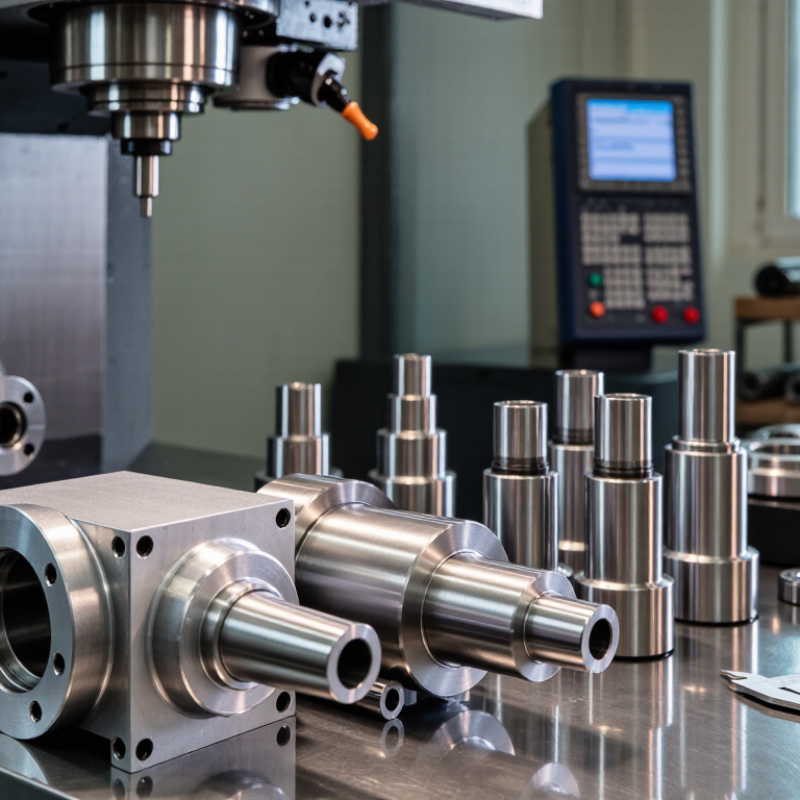
A reliable CNC machining quote starts with a drawing that explains how the part must function. Include a revision number, measurement units, thread specifications, surface finish, and clearly identified inspection datums. For a bearing housing, specify the bore tolerance and its position relative to the mounting face. Dimensions need context. A 0.02 mm tolerance may be necessary for one interface but unnecessarily expensive elsewhere. Blanket tight tolerances can increase machining time, inspection costs, and rejection rates without improving performance.
Tips: Send both a dimensioned drawing and a matching 3D model. Mark critical features, and ask suppliers to flag conflicting requirements before quoting. Check revision consistency. A model alone rarely communicates every manufacturing requirement.
Select materials by grade and condition, rather than broad labels such as “aluminum” or “steel.” Aluminum 6061-T6 can suit many lightweight housings, while 316 stainless steel may suit applications requiring greater corrosion resistance. Actual suitability depends on loads, temperature, exposure, and any applicable industry requirements. Thin walls deserve discussion because clamping forces and residual stress can cause distortion. An initial wall thickness may look practical in CAD yet prove difficult to machine consistently. That assumption deserves review with the supplier. Agree on inspection methods for critical dimensions, and request material certificates when traceability is required.
A machine list tells you little about whether a supplier can repeatedly hold your tolerances. Ask for evidence. Request examples matching your material, geometry, and production volume. For an aluminum housing with ±0.01 mm bores, ask for inspection records from comparable work. Review machine travel, spindle capability, workholding, and temperature control. Five-axis equipment helps with complex access, but programming and fixturing experience still determine results.
The ISO Survey 2022 reported 1,265,216 valid ISO 9001 certificates worldwide, showing how widely quality management systems are adopted. Certification alone cannot demonstrate machining capability for your drawing. Check the certificate’s scope, then examine calibration records, inspection procedures, and recent nonconformance reports. Verify the details. For critical bores, request actual measurements, instrument resolution, and the inspection temperature. A capability index such as Cpk is useful only when the process is stable and the sampling method is credible.
Look for experience with the problems your parts actually present. Thin walls can distort after unclamping; deep pockets can create chatter and chip evacuation problems. Ask how the supplier controls these risks during machining and inspection. A perfect sample can still mislead, especially when its setup differs from the proposed production process. That deserves scrutiny. Review a small pilot batch, including measurements taken after parts leave their fixtures. Ask what failed during development and what changed afterward.
Quality checks should begin before you approve a precision CNC machining supplier. The 2022 ISO Survey reported 1,265,216 ISO 9001 certificates worldwide. Certification is widespread, but it cannot prove that your particular drawing requirements will be met. Request a recent inspection report for a comparable part, with customer details removed. Check whether it records actual measurements, drawing revisions, sampling frequency, and acceptance limits. Ask for evidence. A report showing only “pass” leaves too much hidden.
Match inspection methods to the features that matter. A coordinate measuring machine can evaluate positional tolerances, while a calibrated bore gauge can monitor critical internal diameters. For a 20.000 ±0.010 mm bore, ask how temperature, instrument uncertainty, and sampling affect acceptance decisions. Temperature matters. Request calibration records and measurement-system studies for critical characteristics, especially when tolerances approach the instrument’s practical capability. A capability index looks reassuring, but mixed production conditions can make it misleading. Ask whether the calculation represents a stable process and the same setup planned for your order.
Material traceability needs a physical trail, not just a certificate in an email. Match the material certificate’s heat number to incoming stock labels, production travelers, and finished-part batch records. For aluminum parts, verify the specified alloy and temper, rather than accepting a generic material description. Ask how identification survives when bars become small blanks. This step is easy to underestimate. Even a complete dimensional report cannot establish that the correct material reached the machine.
A low CNC machining quote can hide expensive assumptions. Compare identical drawings, material grades, quantities, and inspection requirements across suppliers. For example, specify 6061-T6 aluminum, a 100-piece batch, and the required surface finish. Ask suppliers to separate setup, machining, finishing, and inspection charges. Check tolerances carefully. A ±0.01 mm requirement may increase machining and inspection costs, so reserve it for functionally critical features. Blanket tight tolerances can make an ordinary bracket unnecessarily expensive.
Tips: Ask whether quoted lead times include material procurement, outside finishing, inspection, and packing. Confirm available production capacity before treating an estimated shipping date as a commitment. A ten-day machining schedule can become four weeks when anodizing queues and material availability enter the picture. Request a dated schedule with clear milestones, especially when your assembly deadline cannot move. Build some buffer. A supplier’s quickest estimate may be achievable, but it leaves little room for rework.
Calculate total sourcing cost using freight, duties where applicable, packaging, currency conversion, and receiving inspection. Divide those costs by the number of usable parts, rather than the quantity ordered. Compare a small pilot batch before committing to recurring production, and request inspection results for critical dimensions. Samples cost extra, and they cannot guarantee every later batch will match. That limitation deserves attention. For repeat orders, document acceptance criteria and clarify who pays for rejected parts, replacement freight, and additional inspection.
A machining quote is only one component of total sourcing cost. This chart shows how two U.S. import fees change with declared merchandise value for non-exempt commercial ocean shipments entered through ports subject to the Harbor Maintenance Fee. Calculations use published fiscal year 2025 fee rates, rather than supplier or brand data.
What the chart shows: The Merchandise Processing Fee is 0.3464% of merchandise value, with a fiscal year 2025 minimum of $32.71 and maximum of $634.62 per formal entry. The Harbor Maintenance Fee is 0.125% of merchandise value. Together, these fees equal $38.96 on a $5,000 shipment and $947.12 on a $250,000 shipment. These are calculated fee amounts, not complete landed-cost estimates.
Apply these seven sourcing checks: (1) Send identical drawings and tolerances to each supplier; (2) confirm material and inspection requirements; (3) separate setup charges from unit prices; (4) compare production lead times; (5) include freight and customs clearance time; (6) calculate duties, processing fees, brokerage, and delivery costs; (7) assess rework and delay exposure before selecting a quote. Customs duties depend on classification, origin, and applicable trade measures and are excluded from this chart.
Sources: U.S. Customs and Border Protection: User Fee Information; 19 CFR § 24.23: Merchandise Processing Fees; 19 CFR § 24.24: Harbor Maintenance Fee. Historical fee schedule: October 1, 2024–September 30, 2025. Merchandise values are calculation scenarios. All amounts are USD; exemptions may apply.
A sample that looks clean can still fail during assembly. Request parts made with the proposed production material, tooling, and finishing process. Check the fit. For a locating bore specified at 10.000 ±0.010 mm, request actual measurements rather than a simple pass mark. Ask the supplier to identify the inspection equipment, measurement conditions, and relevant calibration records. A single approved sample provides useful evidence, but it cannot establish whether the process will remain consistent across batches.
Translate sample findings into written acceptance criteria before placing the production order. Define critical dimensions, datum references, surface roughness, thread requirements, and acceptable cosmetic defects. Make defects visible. Photographs can distinguish an acceptable tool mark from a burr that interferes with assembly. Specify whether dimensions apply before or after finishing, since coatings can change a close fit. For critical features, agree on an inspection method with measurement uncertainty appropriate to the tolerance, plus a sampling plan suited to the consequences of failure.
Keep an approved sample alongside the controlled drawing revision and inspection report. Treat that sample as a reference; numerical requirements still need documented limits. Some judgment remains unavoidable, especially when evaluating appearance under different lighting. That ambiguity deserves attention. If two inspectors disagree, revise the criteria with clearer photographs, viewing conditions, or measurable limits. Require suppliers to flag material substitutions, tooling changes, and process adjustments that could affect previously approved characteristics.
| Validation Area | Sample Part Validation | Example Production Acceptance Criteria | Verification Method | Example Inspection Frequency |
|---|---|---|---|---|
| 1. Confirm Material and Traceability | Review the material certificate and confirm that the sample is linked to the specified alloy, temper, and material lot. | Example material: aluminum alloy 6061-T6. The certificate must identify the specified alloy and temper, and the material lot must remain traceable to the finished parts. | Review material certificates, purchase specifications, and production records. Request independent material testing when required by the purchase specification. | Review documentation for every incoming material lot and verify traceability for every finished production lot. |
| 2. Verify Critical Dimensions | Measure all drawing dimensions on three initial sample parts. Record actual values for critical mating features. | Example bore: Ø10.000 ±0.010 mm, giving an acceptable diameter of 9.990–10.010 mm. Every inspected critical feature must meet its drawing limits. | Use a calibrated bore gauge, air gauge, or suitable coordinate measuring machine. Evaluate instrument suitability and measurement uncertainty. The standard reference temperature for dimensional specifications is 20 °C under ISO 1. | Inspect the first part after setup or adjustment, then inspect the example critical bore on every production part. |
| 3. Check Geometric Accuracy | Validate functional geometry using the drawing's specified datum references and geometric tolerances. | Example mounting-face flatness: ≤0.030 mm. The entire extracted surface must fit between two parallel planes separated by 0.030 mm; flatness does not require a datum. | Use a coordinate measuring machine or a validated surface-plate measurement procedure, with sufficient measurement coverage to evaluate the surface. | Inspect all initial samples, the first production part, and one part every 25 pieces. Contain parts produced since the last accepted check if a failure occurs. |
| 4. Measure Surface Texture | Measure the functional surfaces identified on the drawing and document the measurement direction and instrument settings. | Example sealing-face requirement: Ra ≤1.6 µm. Meet the specified roughness limit using the agreed filtering, evaluation length, measurement direction, and acceptance rule. | Use a calibrated surface roughness instrument. Ra is the arithmetic mean height of the assessed roughness profile; visual inspection alone cannot confirm an Ra value. | Check all initial samples, the first production part, after relevant tool changes, and one part every 25 pieces. |
| 5. Validate Threads and Assembly Fit | Gauge threaded features and verify assembly with the specified mating components or an approved functional fixture. | Example internal thread: M6 × 1-6H. Accept only threads that satisfy the applicable GO/NO-GO gauging rules and the drawing's thread-depth requirement. | Use calibrated thread plug gauges suitable for the specified thread. ISO 1502 provides gauging requirements for ISO general-purpose metric screw threads. | Gauge every example critical threaded hole. Repeat the assembly check after setup changes that could affect fit. |
| 6. Define Edge and Cleanliness Requirements | Inspect accessible edges, hole intersections, and internal passages for burrs, loose chips, and damage. | Example drawing requirement: apply a 0.2–0.5 mm × 45° chamfer to identified edges. No loose chips or attached burrs are permitted on designated assembly and sealing surfaces. | Use visual inspection under defined lighting, magnification where needed, and dimensional measurement of specified chamfers. Use a borescope for inaccessible passages when required. | Inspect every finished part after deburring and cleaning, before protective packaging. |
| 7. Approve Records and Control Changes | Review the sample inspection report against the current drawing revision. Resolve discrepancies and approve a documented production inspection plan. | All required sample results must meet the approved specification. Reports must identify the part, drawing revision, inspected characteristics, results, and measuring equipment. Obtain approval before implementing changes that require customer authorization. | Review the inspection report, calibration status, material records, approved deviations, and change records. Retain an identified reference sample when useful. | Complete approval before production release. Review required records for each shipment and repeat affected validation after relevant changes. |
Application note: Numerical tolerances, material selection, sample quantities, and inspection frequencies above are illustrative purchasing requirements, not measured supplier data or universal industry limits. Confirm them against the actual drawing, functional risks, process capability, and agreed inspection plan. Three conforming samples alone do not establish production process capability. Apply documented decision rules for measurement uncertainty and define lot containment and disposition procedures before production.